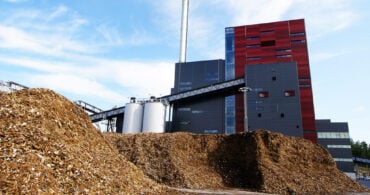
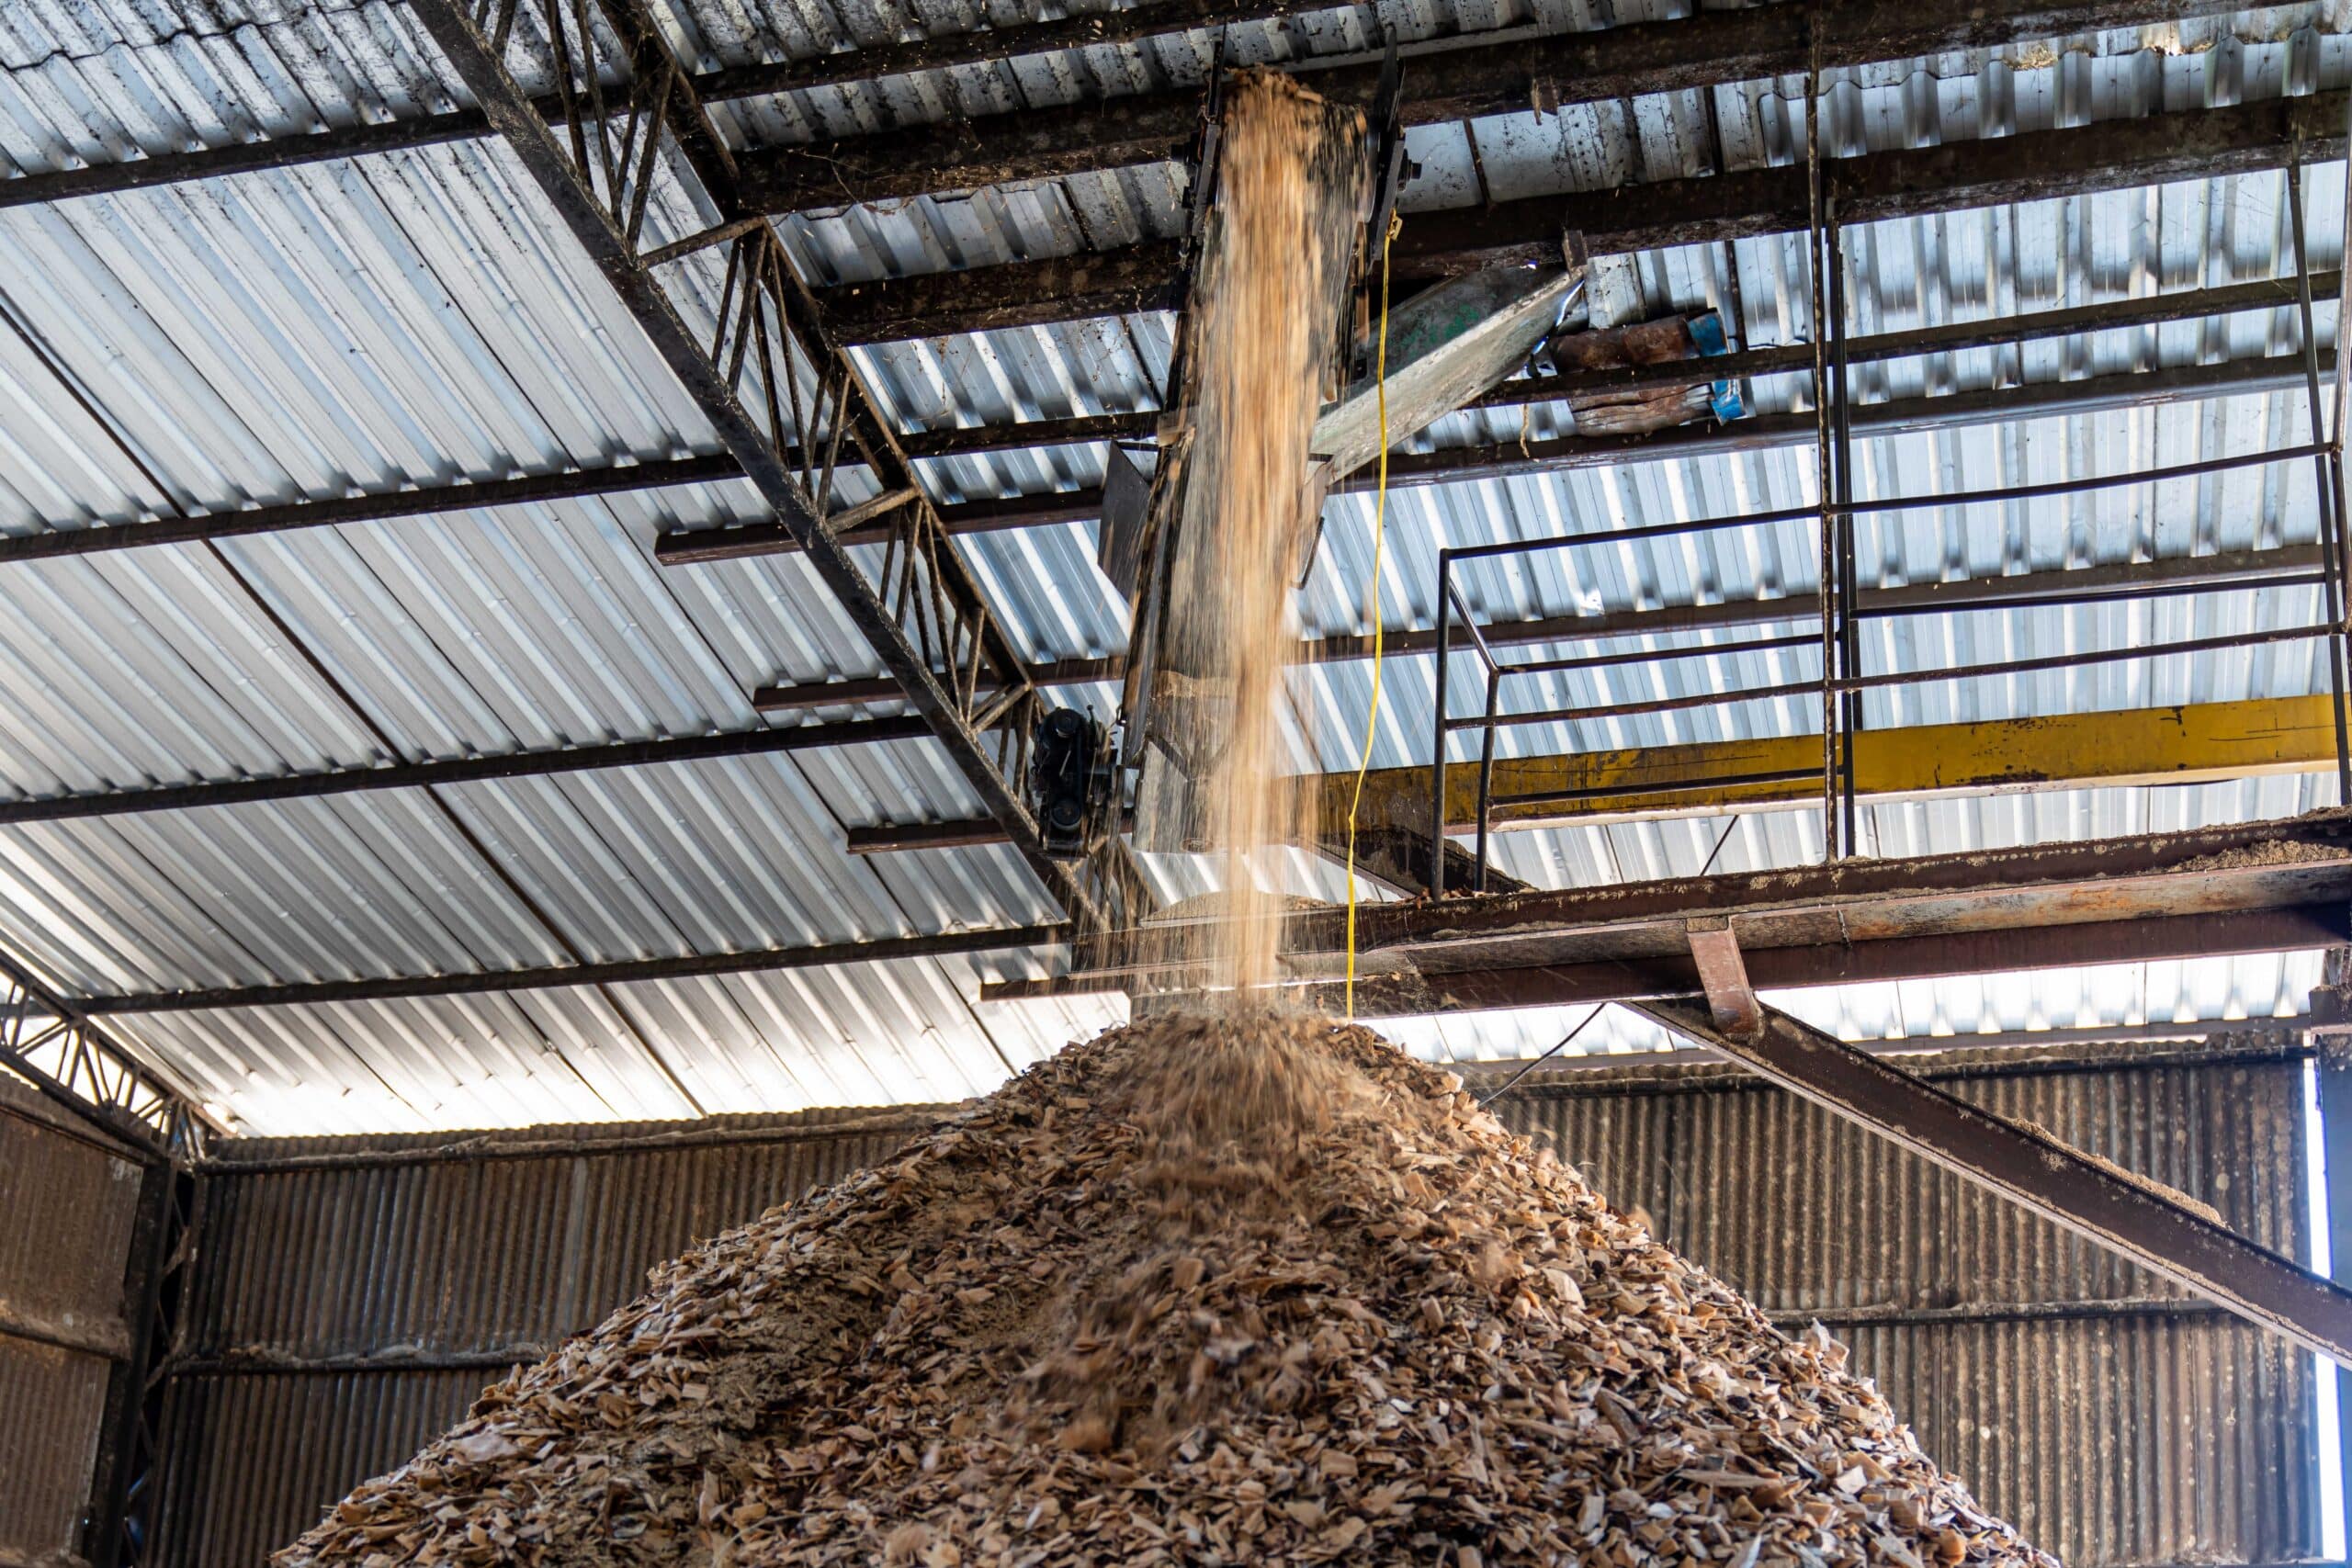
Using biomass as an energy source in industrial boilers has gained ground in recent years as companies look for more sustainable, renewable alternatives. To ensure these systems run efficiently, however, it is essential to monitor and control the moisture of the biomass. In this article we look at why measuring biomass moisture in industrial boilers matters and the benefits this control brings to combustion and overall operation.
The role of moisture in biomass combustion
Moisture is a critical factor in biomass combustion because it directly affects burning efficiency and boiler performance. High-moisture biomass needs more energy to evaporate its water during combustion, which reduces the heat available for steam generation. Excess moisture can also cause smoke, ash deposits and pollutant emissions, hurting the process and environmental compliance.
Benefits of moisture measurement
- Energy efficiency: By measuring and controlling biomass moisture, boiler operation can be optimized for more efficient combustion and maximum steam output. This increases energy efficiency, lowers operating costs and improves profitability.
- Lower emissions: Accurate moisture measurement allows combustion conditions to be adjusted and excess moisture avoided. This reduces pollutants from incomplete combustion, such as carbon monoxide (CO) and particulate matter, supporting regulatory compliance and air quality.
- Ash deposit control: The right moisture content prevents sticky ash that can cause blockages and corrosion. Continuous measurement allows operating parameters to be adjusted, avoiding excessive deposits and extending boiler life.
- Fuel quality: Regular moisture measurement with reliable, accurate meters provides information on fuel quality. Knowing the exact moisture content helps you choose reliable suppliers, avoid overly wet biomass and keep combustion results consistent over time.
Moisture measurement technologies
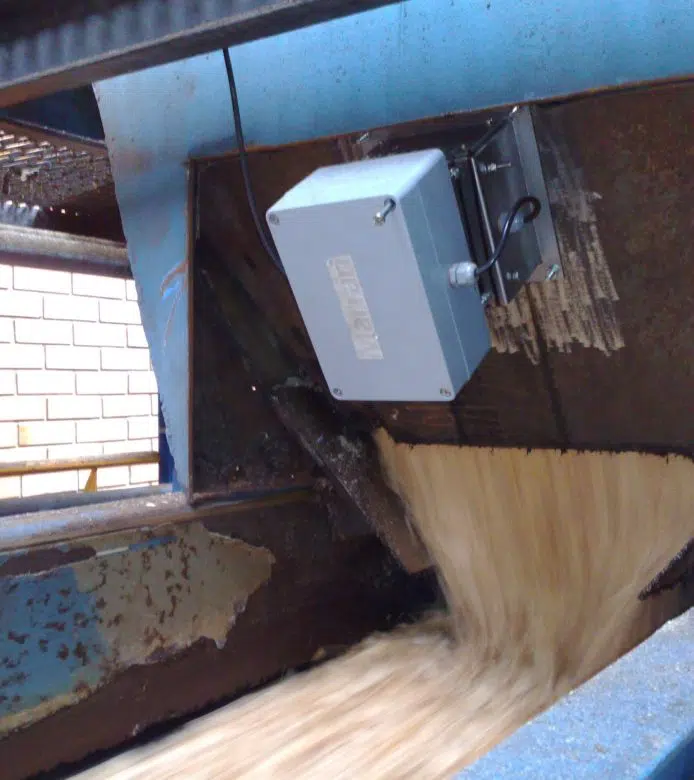
Several technologies are available to measure biomass moisture. Among them, capacitance measurement is one of the most reliable and widely used in industrial boilers. In this method, capacitive sensors are placed in the biomass flow and moisture is estimated from the change in capacitance caused by water. The technique offers continuous real-time measurement, high accuracy, fast response and the ability to monitor moisture at different points in the process. Capacitive systems can also be integrated directly with the boiler for precise, automated moisture control during operation. See UmiChip, Marrari’s in-line biomass moisture meter.
Benefits of capacitance moisture measurement
- Precise moisture control: Capacitance measurement allows precise, real-time control of biomass moisture in the boiler. This enables immediate adjustments, such as feed rate and airflow, to keep moisture within the ideal combustion range and maximize heat and steam generation.
- Lower emissions: Proper moisture control helps reduce emissions. With moisture at ideal levels, combustion is more complete and carbon monoxide (CO) formation is minimized. Excess moisture also produces smoke and particles that pollute the air; capacitance measurement helps control these and meet environmental regulations.
- Preventing combustion problems: Improper moisture can cause incomplete combustion, deposits and corrosion. By continuously monitoring moisture, combustion can be adjusted to biomass variations for more stable, reliable boiler operation.
- Better energy efficiency: Accurate moisture measurement and control make better use of biomass. Wet biomass needs more energy to evaporate water and leaves less heat available; keeping moisture at ideal levels maximizes efficiency and reduces fuel consumption and costs.
It is also important to calibrate measurement equipment regularly to ensure accurate, reliable results.
Conclusion
Measuring biomass moisture in industrial boilers is key to optimizing energy efficiency, reducing emissions, controlling ash deposits and ensuring fuel quality. Continuous monitoring allows operating parameters to be adjusted, minimizing the negative effects of moisture on combustion.
To achieve these benefits, it is essential to invest in reliable moisture measurement technology and a proper maintenance program. Accurate measurement combined with good control leads to more efficient combustion, lower operating costs and greater sustainability.
Want to apply this in your plant?
Talk to a Marrari specialist on WhatsApp or see the right solution for your process.