Why use moisture meters?
The reason to use moisture meters is closely tied to properly managing this vital factor across many industrial sectors. Their importance goes beyond simple measurement: they decisively influence both product quality and process efficiency.
In this article we look at the key reasons why using moisture meters is essential in industry, with a focus on the benefits of capacitive meters.
Quality control and operational efficiency
- Preserving quality: In the food and pharmaceutical industries, maintaining product quality is essential. In drug manufacturing, for example, moisture variations can compromise the chemical stability of active ingredients, making products less effective or even harmful. Moisture control, combined with temperature and pressure monitoring, is therefore essential for safe, high-quality production.
- Avoiding inefficient processes: In sectors such as paper and textiles, where moisture is critical, a lack of control has adverse effects. In papermaking, improper moisture can deform fibers and produce low-quality products. Inefficient drying also lengthens production time and raises costs. Controlling moisture at every stage ensures quality, efficiency and competitiveness.
- Workplace safety: In industrial environments, moisture control also contributes to worker safety. Improper humidity can create conditions for accidents such as slips and falls, so keeping it at proper levels is essential.
- Equipment durability: In sectors such as electronics and manufacturing, excess moisture harms equipment: corrosion and oxidation of components happen faster in humid environments. Good moisture control extends equipment life and lowers maintenance costs.
- Regulatory compliance: Many industries have strict rules on production conditions. Monitoring moisture ensures compliance, avoids fines and penalties, and accurate records help demonstrate it during audits and inspections.
Benefits of using moisture meters in industry
- Saving resources: Moisture control also saves resources. In drying processes, for example, excess moisture lengthens drying time and increases energy use. With accurate data, moisture meters help optimize the use of materials and energy for more efficient and sustainable operations.
- Meeting regulations: In highly regulated sectors such as pharmaceuticals, meeting strict quality and safety standards is crucial. Closely monitoring moisture helps demonstrate that commitment, avoid penalties and keep the trust of customers and regulators.
- Reducing losses: Detecting moisture variations early prevents product damage, such as mold in food or deformation of moisture-sensitive materials. This protects the investment in raw materials, reduces operating losses and makes production more sustainable.
- Energy efficiency: With precise moisture control, HVAC and ventilation systems can be tuned better and use less energy. This lowers operating costs and the carbon footprint.
- Better working conditions: Proper humidity levels create more comfortable conditions for workers, reduce respiratory discomfort and promote a healthier, more productive workplace.
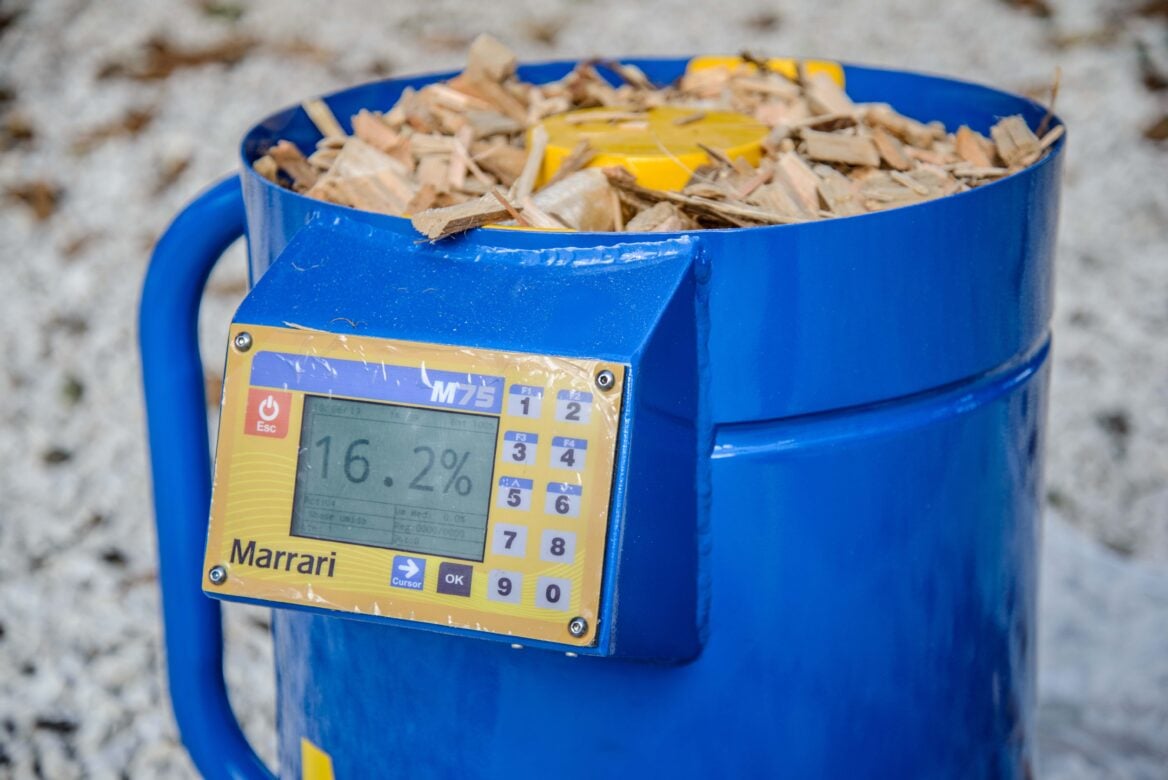
Capacitive meters: the smart choice
- High sensitivity: Capacitive meters accurately detect minimal moisture variations, even in demanding conditions. That sensitivity ensures precise control in industries where a small variation affects quality and efficiency.
- Fast response: Capacitive readings respond quickly, which is essential in dynamic industrial environments that require immediate adjustments. Real-time information supports fast decisions and keeps moisture within target limits.
- Rugged for industrial environments: These meters are built to withstand dust, vibration and wide temperature swings, delivering consistent, reliable operation even where other devices might fail.
- Easy integration: Capacitive meters integrate easily with automation systems and industrial networks, making it simpler to build complete control solutions across the production chain.
- Efficient maintenance: Their durability and reliability reduce the need for repairs and the cost of preventive and corrective maintenance, with less downtime and more stable production.
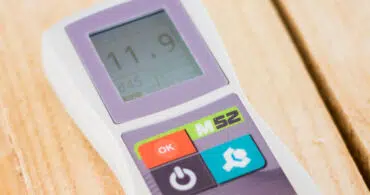
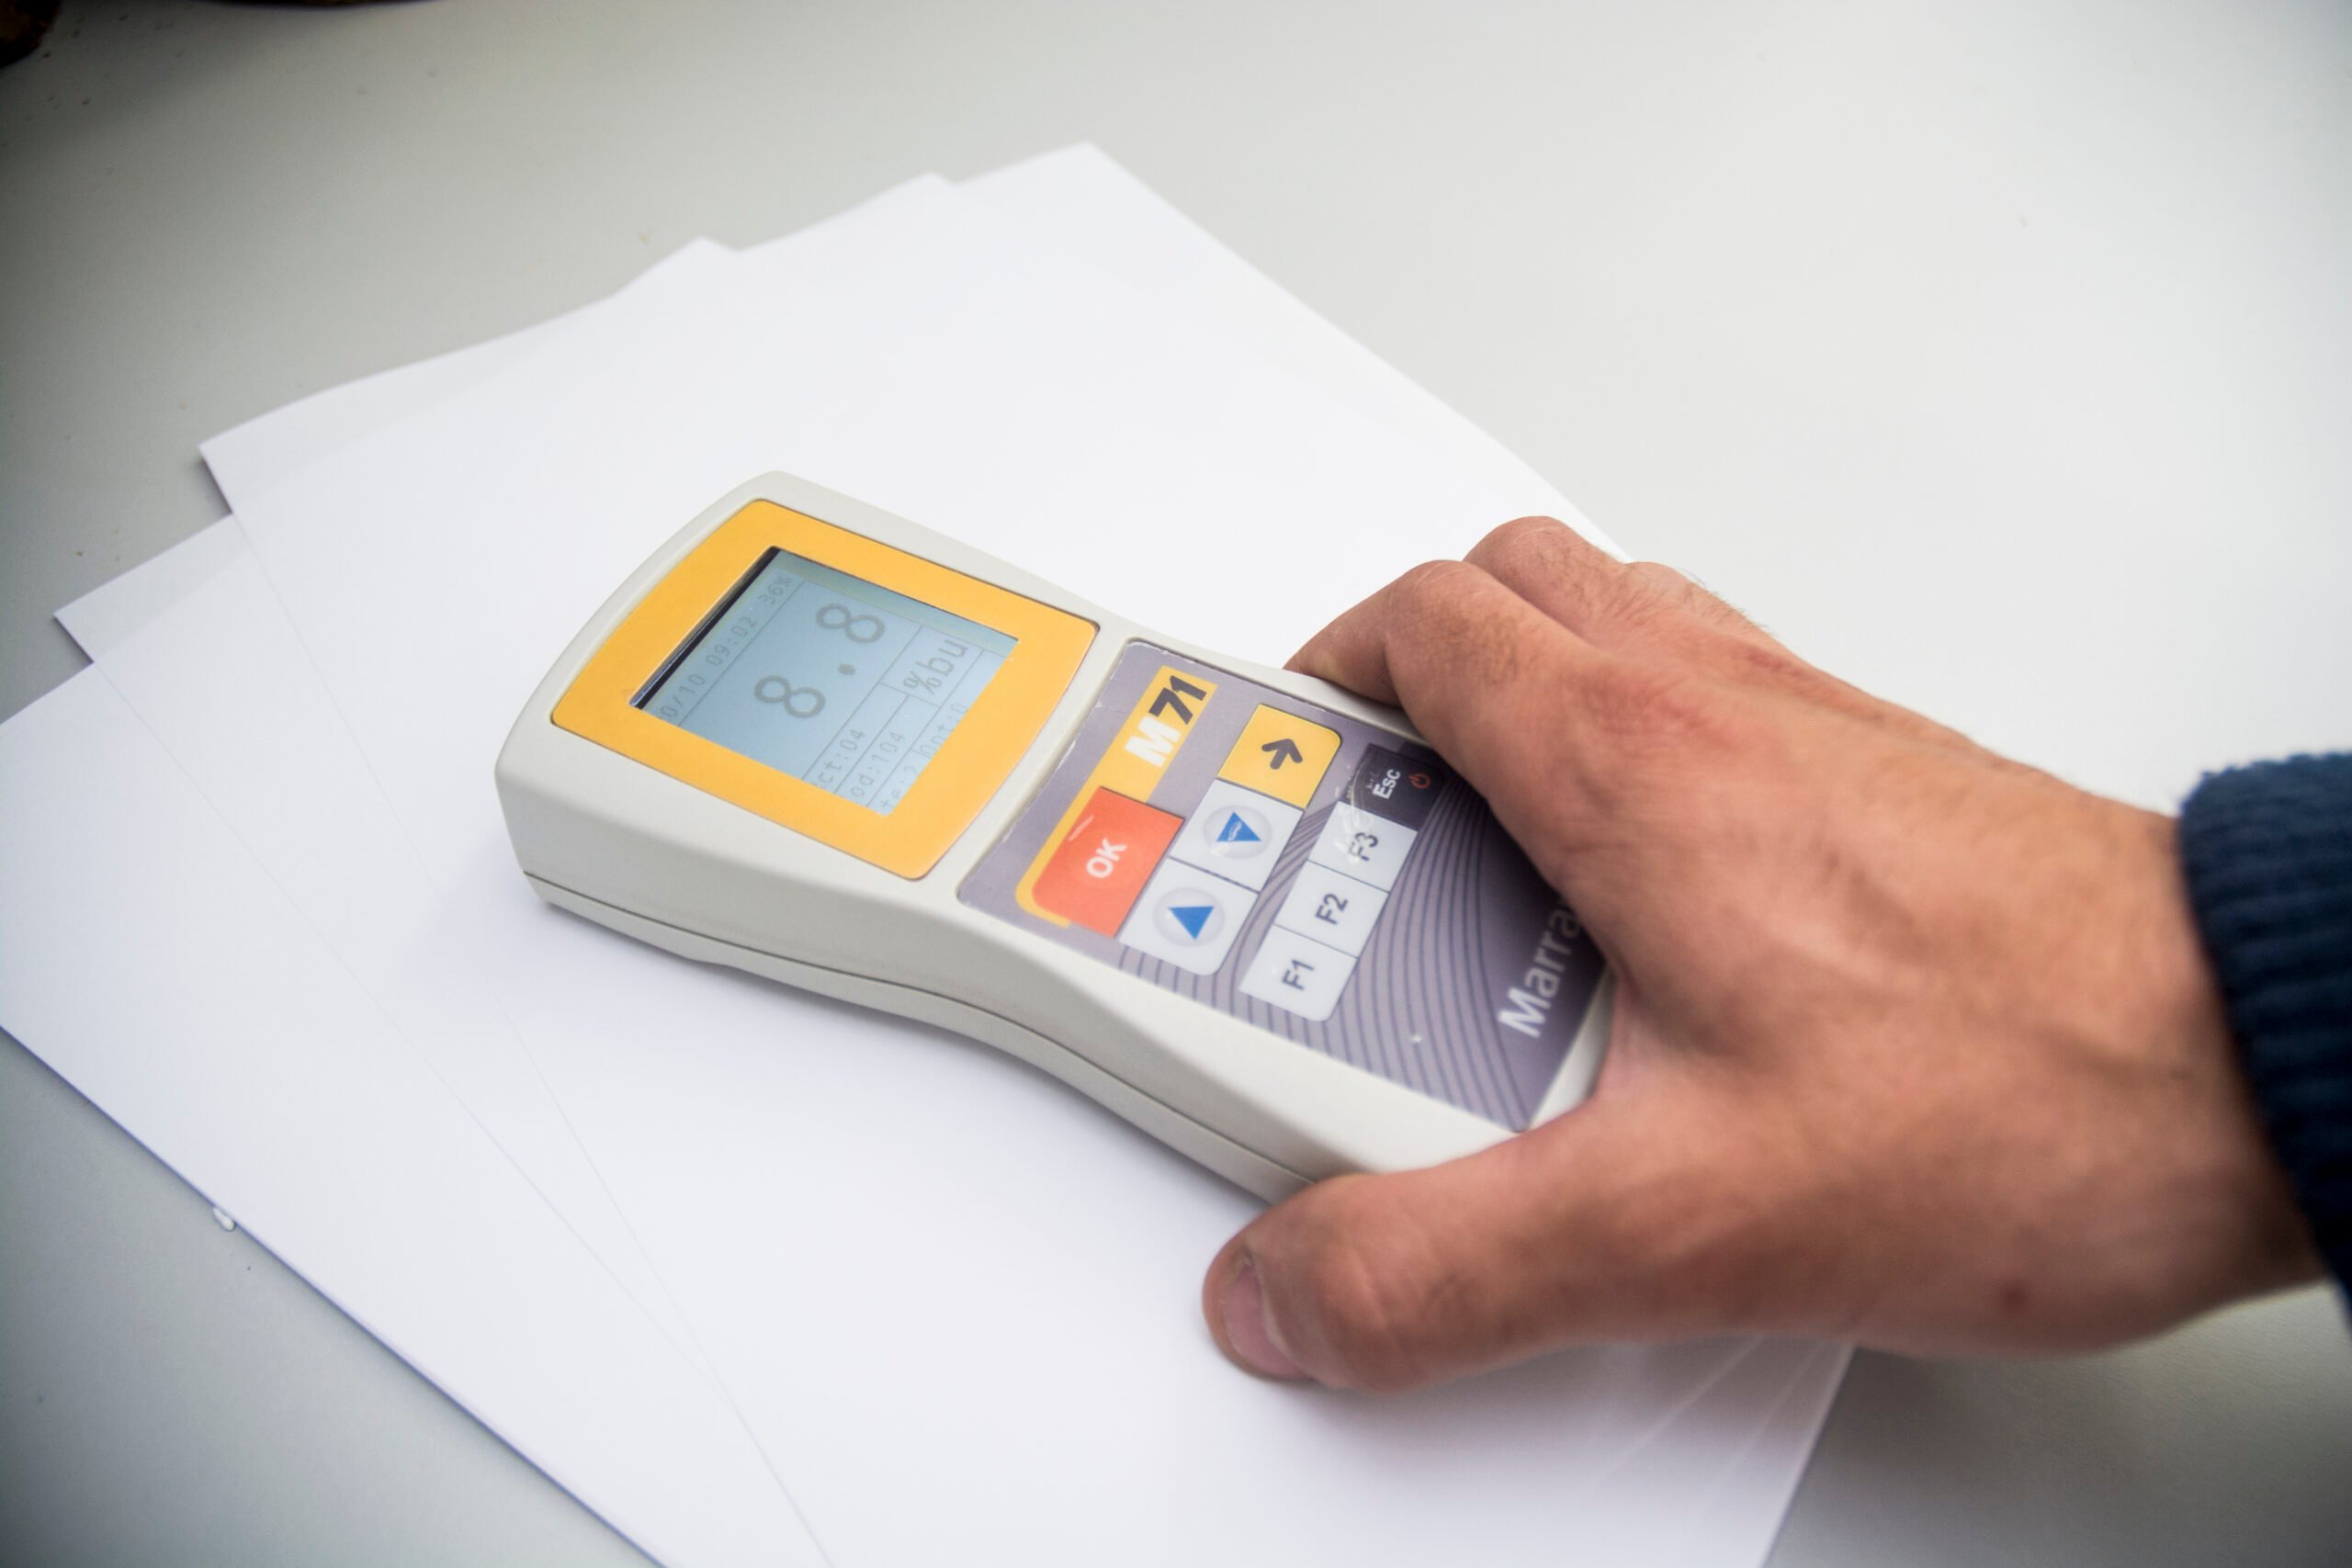
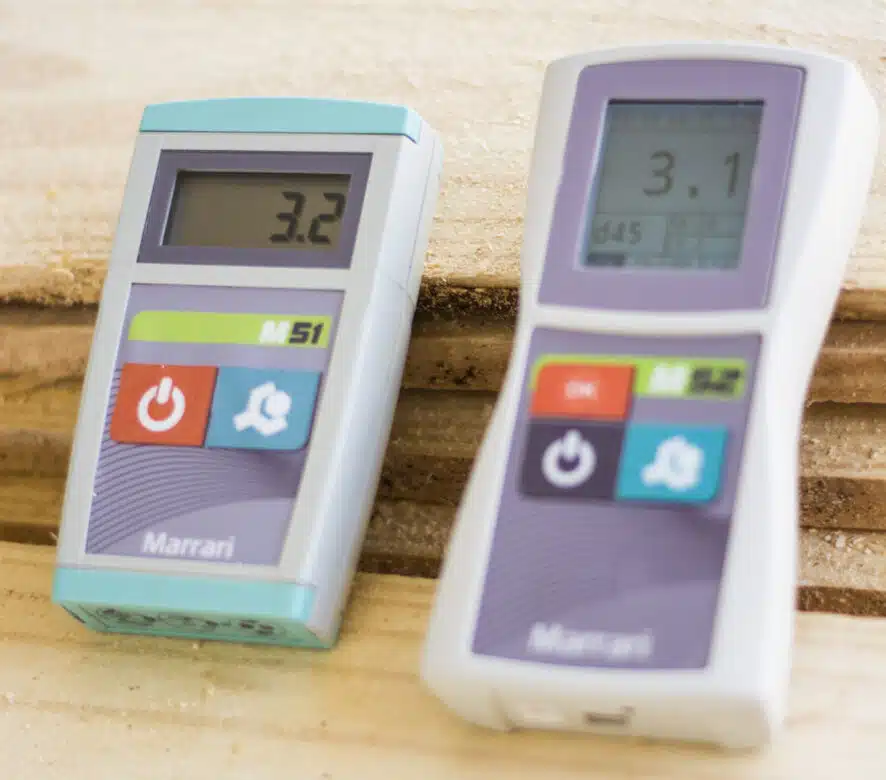
See Marrari’s portable moisture meters for many industrial sectors
Integration in the Industry 4.0 era
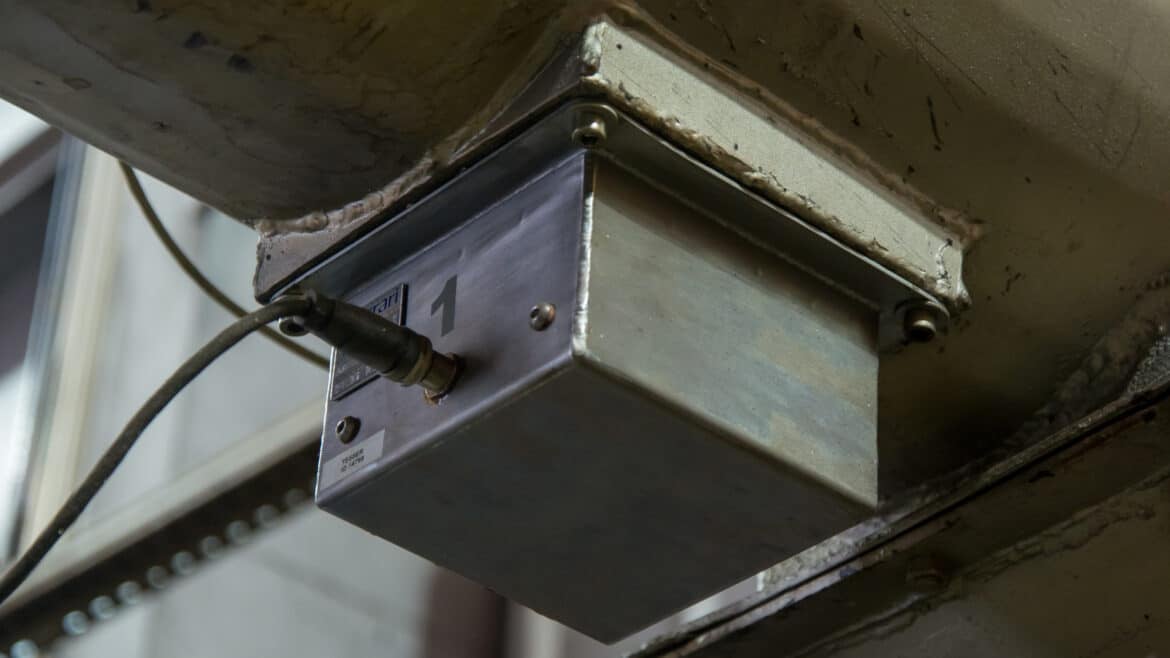
With Industry 4.0, integrating moisture meters becomes strategic for the digital transformation of operations. Real-time data collection and analysis enable predictive strategies, anticipating moisture variations and acting before problems occur, and also support preventive maintenance. See also Marrari’s in-line moisture measurement solutions.
Conclusion
In short, using moisture meters in industry is essential to ensure operational efficiency, product quality and regulatory compliance. Capacitive meters are a smart choice for companies seeking excellence in moisture control.
Want to apply this in your plant?
Talk to a Marrari specialist on WhatsApp or see the right solution for your process.